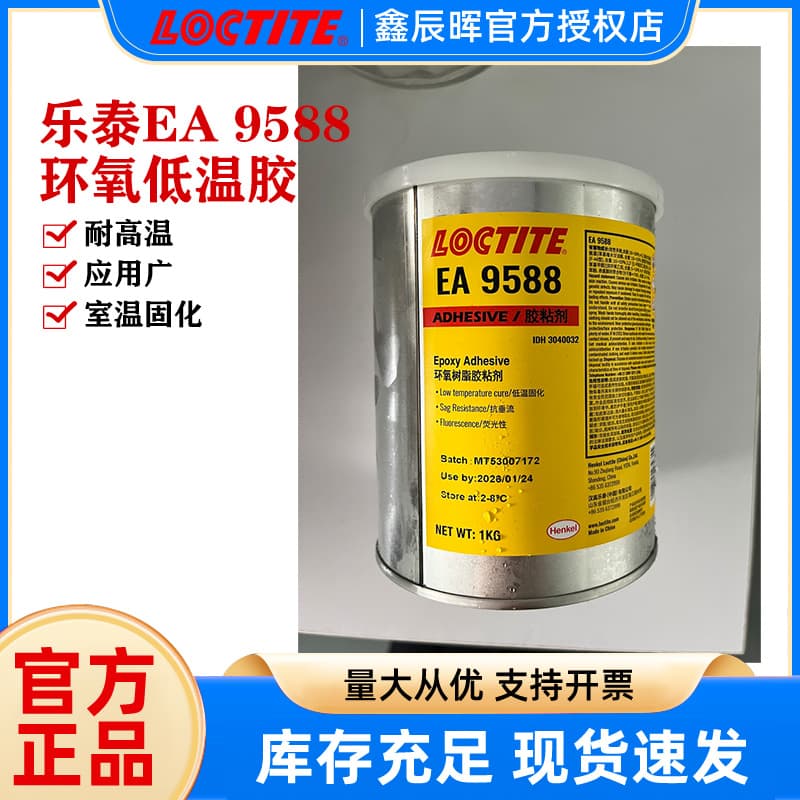
E Loctite EA 9588 Heat cure Epoxy January 2025 RODUCT DESCRIPTION ctite EA9588 is one component heatcure epoxyhesive specifically designed for structure bondingplication.The liquid material has proper viscosity andixotropic property,which makes it easy to apply andg resistance. e adhesive can be cured at 80℃.The cured materialowed good bonding strength to several substrates.Jorescence is another property of this adhesive,whichakes both liquid and cured adhesive be fluorescencetection. cured adhesive provides the following characteristics: chnologyEpoxypearanceBlack liquidomponentsSingle-componentureHeat curescositv @25℃ 1rpm85000-125000scositv @25℃ 10rpm50000-90000 red adhesive provides the below property: chnologyEpoxyass transition temperature/℃SC106.8ecommended curinghedule80℃ for 0.5hourardeness/Sh-D87p shear/Mpa(80℃,0.5hour)-414.0ainless steel9.5alvanized steel11.4ckel coated steel8.8 ORAGE:2-8℃ ENERAL INFORMATION is product is not recommended for use in pure oxygend/or oxygen rich systems and should not be selecteda sealant for chlorine or other strong oxidisingaterials. ote:This product reacts quickly when exposed tomperatures above 80℃.The product evolves heatxotherms)during the solidification reaction. RECTIONS FOR USE sk of stress cracking when exposed to liquid adhesive.cess adhesive can be wiped away with isopropanollvent.Bonds should be allowed to cool before subjecting to any service loads.For specific shelf-lifeinformation,contact your local Technical Service Center. DATA RANGES The data contained herein may be reported as a typicalvalue and/or range.Values are based on actual testdata and are verified on a periodic basis. DIRECTIONS FOR USE 1.For high strength structural bonds,paint,oxide films,oils,dust,mold release agents and all other surfacecontaminates must be completely removed.However,the amount of surface preparation directly depends onthe required bond strength and the environmental agingresistance desired by the user.For specific surfacepreparations on common substrates,see the followingsection of Surface Preparation. 2.Use gloves to minimize skin contact.DO NOT usesolvents for cleaning hands. 3.For maximum bond strength apply adhesive evenly toboth surfaces to be joined. 4.Join the adhesive coated surfaces and allow to cure at80℃ or above until completely firm. 5.Keep parts from moving during cure.Contact pressureis necessary.Maximum shear strength is obtained with a3-5 mil bond line. 6.Excess uncured adhesive can be cleaned up withketone type solvents. DISCLAIMERS This product is experimental only.It is not now and maynever be commercially available. This product is not recommended for use in pure oxygenand/or oxygen rich systems and should not be selectedfor use with chlorine or other strong oxidizing materialsunless otherwise specifically stated. NOTE The data contained herein are furnished for informationonly and are believed to bereliable.We cannot assumeresponsibility for the results obtained by others overwhose methods we have no control.It is the user'sresponsibility to determine suitability for the user'spurpose of any production methods mentioned hereinand to adopt such precautions as may be advisable forthe protection of property and of persons against anyhazards that may be involved in the handling and usethereof in light of the foregoing,Henkel Corporationspecifically disclaims all warranties expressed or implied,including warranties of merchantability or fitness for a
|
 中文
 English